Freezer Load Rejection and What to Do Next
A freezer load rejection rarely begins at the receiving dock. By the time a receiver checks the product temperature, packaging condition or delivery paperwork, the issue may have started during loading, vehicle pre-cooling, a delayed handover or an unplanned stop. For food businesses, freezer load rejection can mean lost stock, disrupted production, missed customer orders […]
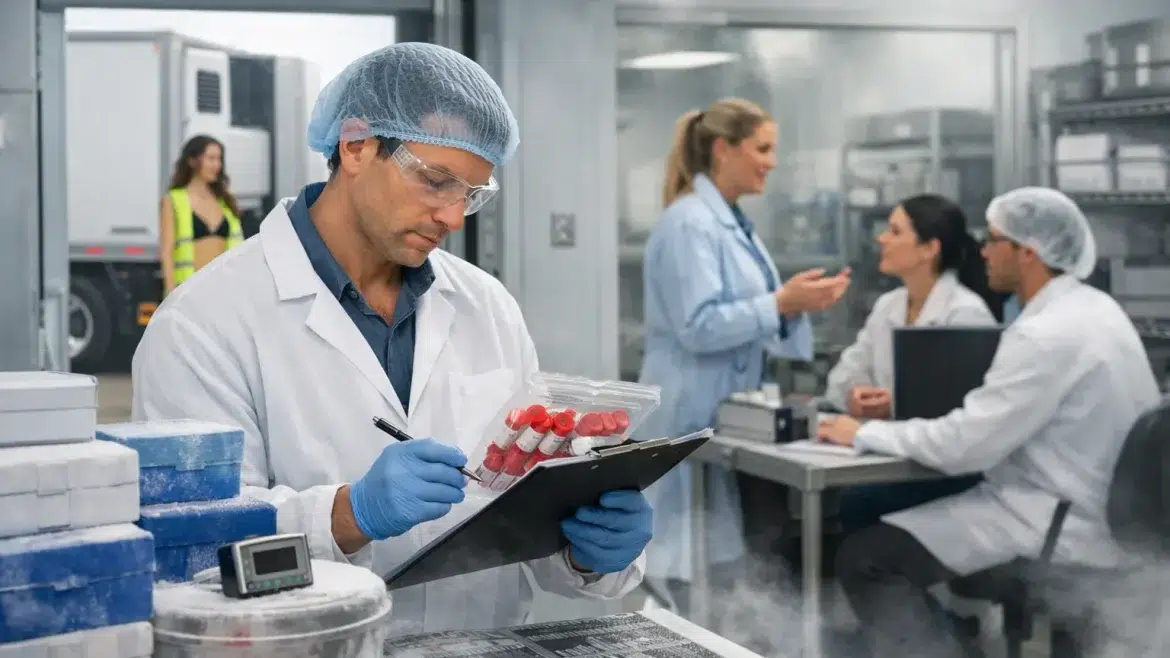
A freezer load rejection rarely begins at the receiving dock. By the time a receiver checks the product temperature, packaging condition or delivery paperwork, the issue may have started during loading, vehicle pre-cooling, a delayed handover or an unplanned stop. For food businesses, freezer load rejection can mean lost stock, disrupted production, missed customer orders and a difficult conversation about who carries the cost.
The best response is not simply to get the load moving again. It is to protect product integrity, establish the facts quickly and prevent the same failure from reaching the next delivery.
What is freezer load rejection?
A freezer load is rejected when the receiving customer decides the freight does not meet its agreed acceptance requirements. Temperature is often the main reason, but it is not the only one. A receiver may reject stock because cartons are wet, crushed or contaminated, pallets are unstable, seals are broken, labels do not match the paperwork, or the vehicle arrives outside the booked delivery window.
For frozen food, the product specification and customer agreement determine what is acceptable. Many products are carried and received at or below -18°C, but the required set point, permitted tolerance and method of temperature checking can differ by product and site. A vehicle display alone may not settle a dispute. Receivers may check product surface temperature, probe a sample, review a temperature record or inspect the load for signs of thawing and refreezing.
That is why freezer transport requires more than setting the unit to the right temperature. It requires controlled handling from dispatch through to proof of delivery.
Why rejected freezer freight is costly
The immediate cost can be substantial. Stock may need to be held, returned, assessed or disposed of. Replacement freight may need to be picked, loaded and dispatched at short notice. If the delivery was supporting a production run, retail promotion or hospitality order, the commercial impact can extend well beyond the value of the affected pallets.
There is also a chain-of-custody issue. Once a receiver has rejected stock, it should not be redirected or released without clear instruction from the owner of the goods. The product may still be safe and within specification, but that decision needs to be supported by evidence and made by the appropriate party.
For suppliers, repeated rejections can affect service levels, customer confidence and future supply arrangements. For carriers, they create avoidable waiting time, redelivery costs and pressure on vehicle availability. Prevention is the most reliable way to protect both the product and the relationship.
The common causes of freezer load rejection
A temperature exception can occur even when the refrigeration unit is operating. Loading warm stock into a cold vehicle, leaving doors open too long, poor airflow around pallets and repeated multi-drop access can all place pressure on the cold chain. Product needs to be at its required dispatch temperature before loading. A refrigerated truck is designed to maintain temperature, not rapidly pull down warm product.
Vehicle preparation matters just as much. The load space should be clean, dry, odour-free and pre-cooled to suit the product requirement before freight is loaded. If the vehicle has been used for another freight type, the condition of the load space must still meet food transport expectations. Condensation, damaged flooring or residue can lead to a rejection even when the temperature is correct.
Packaging and pallet presentation are another frequent issue. Torn cartons, exposed product, collapsed corners and loose stretch wrap can result from weak pallet build, unsuitable loading practices or shifting in transit. Frozen cartons can become particularly vulnerable when they have absorbed moisture or have been handled roughly through multiple transfers.
Documentation can also stop a delivery. Incorrect pallet counts, missing consignment details, unclear temperature instructions or an unsigned proof of delivery create doubt at the point of handover. In time-critical freight, a simple paperwork error can turn an otherwise successful run into a rejected load.
Prevent rejection before the truck arrives
Prevention starts with a clear booking. The transport provider needs accurate information about product type, required carrying temperature, number of pallets or cartons, collection and delivery times, site restrictions, and whether the delivery requires a tailgate lifter. This allows the right vehicle, equipment and service window to be allocated from the beginning.
At collection, the sender should confirm the freight is ready for transport. That includes checking product temperature where required, ensuring cartons are sealed and labels are legible, and making sure pallets are stable enough for handling. The freight should not be left in an uncontrolled area while waiting for collection. Small delays at the dock can have a larger effect when several collections or deliveries are scheduled on the same run.
Inside the vehicle, pallets need to be positioned to support airflow and secure travel. Overpacking the load space or placing freight hard against areas needed for air circulation can create uneven conditions. Doors should remain closed whenever practical, particularly during warm weather and at sites with slow receiving processes.
Temperature monitoringprovides an important record, but it is not a substitute for good handling. A monitored journey can show what occurred during transit and help resolve questions quickly. It cannot correct freight that was loaded out of specification or packaging that was already compromised.
Match the service to the delivery conditions
Not every freezer job has the same risk profile. A direct, full-pallet delivery to a site with a fast receiving dock is different from a multi-drop run involving limited access, strict booking times and manual unloading. The service plan should reflect that difference.
For example, a tailgate-equipped truck may be essential where there is no loading dock.Overnight or weekend deliverymay reduce congestion and help meet a narrow receiving window. A flexible collection time may be useful when a production schedule changes, but it still needs to allow enough time for the goods to be properly frozen, checked and staged.
The lowest freight rate is not always the lowest overall cost if the service does not match the product and site requirements. Clear quoting, including any waiting time, extra drops or special handling needs, helps avoid decisions that increase rejection risk later.
What to do when a freezer load is rejected
When a rejection occurs, act promptly but avoid assumptions. The driver should record the time, location, receiver’s reason for rejection and any temperature readings provided. Photographs of packaging, pallets and relevant vehicle conditions can be useful where permitted. The delivery paperwork should clearly show that the freight was refused, rather than appearing as a completed delivery.
The next step is to protect the goods. Keep the load under the required temperature control while the freight owner, receiver and transport provider agree on instructions. Depending on the circumstances, the freight may be returned, held at an approved location, inspected or redirected. Do not treat rejected product as ordinary available stock.
Evidence should be reviewed together. This may include temperature-monitoring records, vehicle set point, collection and arrival times, loading checks, photographs, receiver records and consignment documentation. The purpose is to establish what happened, not to allocate blame before the facts are known.
If the issue is confirmed, identify the operational change required. It may be a revised loading process, clearer delivery instructions, different packaging, additional time at collection or a more suitable vehicle configuration. A rejection that is handled well can still strengthen the process, provided the corrective action is specific and followed through.
Build a transport process that stands up at the dock
Reliable freezer freight depends on shared discipline. The sender prepares stock correctly. The carrier provides clean, suitable equipment, trained drivers and documented temperature control. The receiver applies consistent acceptance checks and communicates any issue at the time of delivery.
For businesses moving frozen food across Brisbane and South East Queensland,choosing a specialist carrierwith monitored equipment, food-focused handling practices and responsive dispatch support reduces the number of variables that can go wrong. BFC Logistics works with customers to align collection timing, vehicle capability and delivery requirements before freight is on the road.
A rejected load is not just a transport problem. It is a product-integrity event with commercial consequences. Clear instructions, careful loading and evidence-led handling give every freezer delivery the best chance of being accepted without delay.
Post navigation
NEED TEMPERATURE-CONTROLLED TRANSPORT?
Talk to BFC about your freight, delivery window and temperature requirements.
Request a quote